What Is the Best MCB Assembly Robot in 2026?
Choosing the best Mcb Assembly Robot in 2026 is not a contest of headline cycle times. The right system must match your breaker design, production volume, changeover frequency, and quality controls. A robot that places components quickly may still struggle with delicate parts, inconsistent feeding, or frequent model changes. Small details matter: a camera checking contact alignment, a servo press recording force, and a feeder that avoids part jams.
For transparency, the following quotation is editorially composed, not a verified statement from a real person. It is attributed to fictional MCB automation specialist Elena Morris: “A strong assembly robot proves its value in repeatable quality, not speed alone.” That matters. Treat the line as a selection principle, not an industry endorsement.
This guide compares what buyers should examine in a Mcb Assembly Robot, including process fit, accuracy, tooling, software, safety features, service support, and measurable production data. Ask vendors to demonstrate your actual product, not just a polished sample. Review changeover time and reject handling. Check whether inspection results and press-force records can be retrieved later. Not just speed.
No single machine is best for every factory. A high-output line may need integrated feeding and inspection, while a smaller plant may value flexible tooling and simpler operation. Some specifications look impressive on paper. Real production can be less tidy. The most useful choice is the one that performs reliably under your actual parts, operators, and shift conditions.
What an MCB Assembly Robot Builds: IEC 60898-1 Covers Ratings up to 125 A and 25 kA
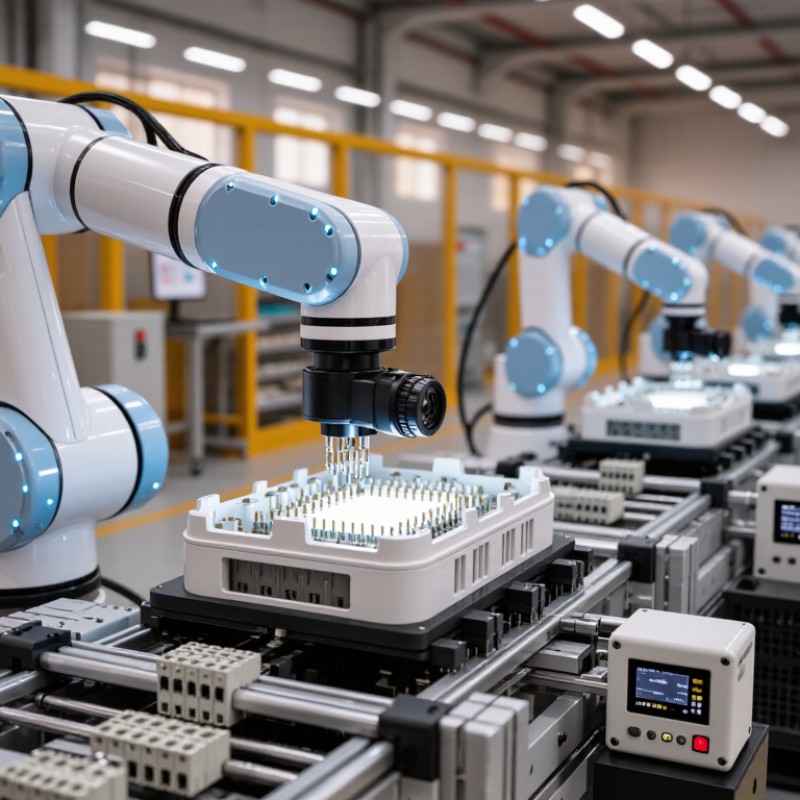
An MCB assembly robot builds miniature circuit breakers from carefully positioned parts: a molded case, contacts, an operating mechanism, and thermal and magnetic trip components. It may feed springs into place, fasten terminals, and check that moving parts travel smoothly. Small details matter. A spring seated slightly out of position can affect later performance.
IEC 60898-1 applies to specified circuit-breakers for household and similar installations. Its scope includes rated currents up to 125 A and rated short-circuit capacities up to 25 kA. These are upper limits in the standard’s scope, not ratings every MCB automatically meets. The actual current and breaking capacity must be declared and verified for each design. That distinction is easy to overlook.
A capable assembly line can control screw torque, monitor component presence, and record test results. It can also support checks of trip behavior and electrical insulation, where the product design requires them. Still, automation alone does not prove conformity. Samples need appropriate testing, and process data needs review. No line is perfect. Even a clear sensor reading may miss a subtle mechanical defect, so careful inspection and validated test methods remain important.
How the Assembly Cell Works: Feeding, Contact Assembly, Calibration, and Testing
What Is the Best MCB Assembly Robot in 2026?
How the Assembly Cell Works: Feeding, Contact Assembly, Calibration, and Testing
A capable MCB assembly cell starts with controlled feeding. Vibratory bowls or step feeders orient housings and small metal contacts, then deliver them to the workstations. Sensors check position before a robot picks each part. A misplaced contact can damage a housing, so reliable detection matters as much as speed. Smooth feeding prevents jams.
At the contact station, a robot places moving and fixed contacts into the molded case. Force monitoring helps confirm that each part seats correctly. Cameras can verify orientation, while a press records insertion depth. Small variations in parts still happen. The cell needs clear limits and a safe way to pause for inspection, not just faster motion.
Calibration sets the mechanism’s trip characteristics, including the force or travel needed to operate. Test equipment then checks electrical continuity, insulation, and trip response against the product’s specified requirements. Results should be linked to each unit, so teams can trace failures to a station or process change. A good robot is not automatically the best cell. Changeover time, measurement consistency, reject handling, and maintenance access matter too. No system is perfect. A sensor threshold may reject a borderline unit that would pass a repeat check; reviewing those cases helps refine the process without weakening quality controls.
Which 2026 Metrics Matter: Cycle Time, OEE, Yield, and Changeover Time
In 2026, choosing an MCB assembly robot means comparing more than its advertised speed. Cycle time should be measured across a complete, verified unit, including loading, component placement, inspection, and discharge. A machine that finishes quickly but pauses for frequent resets may miss its production target. Watch a full shift, not only a polished demonstration.
OEE helps reveal those hidden losses. Record availability, performance, and quality using the same production window, then check downtime logs against operator notes. Small stoppages matter. A feeder that jams for two minutes repeatedly can erode output more than one planned service pause. Yield also needs context: track first-pass good units and rework separately, especially after tooling adjustments or a new component lot. Clean data matters.
Changeover time deserves a practical test. Start the clock when the last good unit leaves one configuration, and stop when the next configuration produces stable, accepted units—not merely the first piece. Include recipe selection, fixture swaps, sensor checks, and trial runs. Ask technicians to repeat the changeover without engineering help. That may expose a weak point. No single metric tells the whole story, and site conditions can make a benchmark look better than daily reality. Compare like-for-like product mixes, shifts, and quality criteria before deciding which cell fits your line.
How to Select a Best-Fit Cell for MCBs Rated up to 440 V under IEC 60898-1
The best MCB assembly robot in 2026 is the cell that matches your product range, not the one with the most axes. For MCBs rated up to 440 V, start by mapping pole counts, housing dimensions, terminal styles, and assembly steps. Check that the feeder handles each part without scuffing insulation or mixing similar components. Small mistakes matter.
IEC 60898-1 provides a product framework, but a robot cell does not prove compliance by itself. Plan for controlled screwdriving, force monitoring, and checks for missing or reversed parts. Add vision where terminals or markings need confirmation. Keep electrical and mechanical verification stages distinct, and confirm the test plan with qualified compliance specialists. Record process settings and inspection results for each production batch.
Run sample builds across the full product range before choosing a layout. Watch changeover time, jam recovery, and access for maintenance; these often matter more than advertised cycle speed. A clear operator screen helps, too. Keep it simple. No cell fits every factory perfectly. Even a well-designed setup may need adjustments after real parts reveal variation in molding, terminals, or component feeding. Ask suppliers to demonstrate those edge cases using your actual MCB components.
What Is the Best MCB Assembly Robot in 2026? How to Select a Best-Fit Cell for MCBs Rated up to 440 V under IEC 60898-1
Voltage reference points for defining the product range a prospective assembly cell must handle.
How to use this: 230 V and 400 V are nominal voltage references for common low-voltage systems; 440 V is the upper rated-voltage scope between phases in IEC 60898-1. These are voltage references, not robot performance ratings. Select the cell against the exact MCB configuration, including poles, rated current, breaking capacity, trip curve, and required assembly processes.
References: IEC 60898-1 scope; IEC 60038 nominal system voltages.